 English
 简体中文
 Español
 Русский
 Português
 العربية
- Cosmetics
- Nouvelle-Zélande
- 2025
Valve position drift on a filling line
Valve position drift is the fault nobody watches happen. On a New Zealand skincare line it was being found the same way every time — in a batch that had already been made, filled and set aside.
Where the valve sits
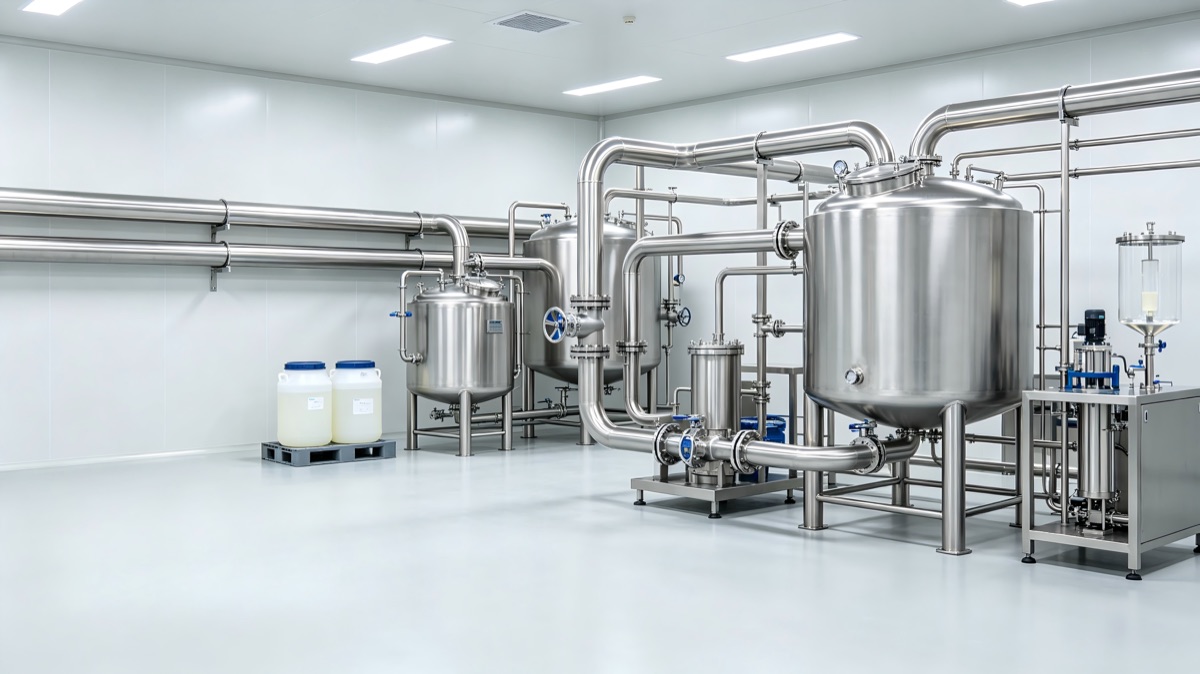
High-end skincare is made to a cleanliness standard closer to pharmaceutical than to food. Raw materials are emulsified and homogenised, and the semi-finished product is held. The filling heads then dose it into containers, which have to carry the same weight and the same product as the ones before them. Every stage is under hygienic control, and every stage depends on flow and pressure being what the recipe says they are.
This customer develops and makes its own skincare range in New Zealand. It runs on one automated line that emulsifies at one end and fills at the other. Changeovers between products are frequent, which is what a brand with a catalogue does. Every one of them is a chance for the line to come back slightly different from how it went away.
What valve position drift costs
The valves on the line were conventional pneumatic ones, set by hand or through a mechanical positioner. That arrangement has a ceiling on how precisely it can hold an opening, and the ceiling moves. Air supply pressure fluctuates and linkages wear. The position the valve actually takes drifts away from the position it was commanded to take.
Drift alone would be manageable if anybody could see it. A mechanical positioner cannot tell you anything about itself. It does not know its seal is ageing, and it does not know it is sitting two degrees off. Either way it has no means of saying so. So the first evidence of a problem was a finished batch that did not match the one before it. The investigation then ran backwards — through records, through retained samples, through the line — to arrive at a valve.
For a product at this end of the market that is worse than a production cost. Batch-to-batch variation in a skincare range is something customers notice and a brand cannot afford. The hours spent reconstructing what happened are hours nobody planned for. On top of it, every changeover meant walking the line and re-checking valves by hand, because nothing on the line could confirm its own setup.
What we supplied
Sanitary valves fitted with our own intelligent positioner, which is really three things the mechanical one could not do.
It senses position rather than assuming it. A high-precision sensor reads where the valve actually is, and the control algorithm holds it there against whatever the air supply is doing that afternoon. Flow control through emulsification and filling tightened as a direct consequence, and consistency between batches with it.
It sets itself up. On commissioning the positioner identifies the valve it is mounted on and configures itself. The manual mechanical adjustment that used to be repeated at every product change is simply not part of a changeover any more. A line that changes product often gets that time back every time.
And it reports. Position deviation, sealing behaviour and air supply pressure are monitored continuously. A seal going off or a valve beginning to drift shows up as a reading that has moved. That is days before it would have shown up as a batch to quarantine. The valves themselves are seat-tested under pressure testing before they leave. What the positioner is holding is a valve that was tight when it shipped.
What it changed
The line started finding its own faults instead of the laboratory finding them afterwards.
Control precision on the filling end improved, and batch-to-batch consistency with it. Changeovers stopped including a manual round of valve checks, so the line switches product faster and the switch is repeatable rather than re-negotiated each time. The unplanned stops that used to follow a bad batch — the investigation, the re-clean, the re-run — largely stopped happening. Those conditions are now caught while they are still conditions.
The maintenance change is the quiet one. The plant went from repairing valves that had failed to servicing valves that had said they were about to.
Why this one came to us
The positioner is ours, and it was designed against sanitary valves rather than adapted to them. That matters more than it sounds. An industrial positioner assumes a valve that is never taken apart, and a sanitary valve is taken apart and put back constantly.
What this side of the work asks for is three things at once. Cleanliness the plant can demonstrate, traceability that survives an audit, and batch records that agree with each other. We work back from those rather than forward from a valve catalogue. So this was a conversation about selection, body design, and how the positioner would talk to the line's control system. The quotation came afterwards.
What the customer bought was not a valve. It was a line that stays where it was set.
Cela se produit-il sur votre ligne ?
Indiquez-nous la dimension, le raccordement et le fluide, et vous recevrez une offre chiffrée plutôt qu’une demande de précisions.
D’autres lignes comme celle-ci
-
Brewing
Butterfly valve stem lift in a brewery
-
Dairy
Stainless steel rusting in coastal air
-
Émirats arabes unis
Manifold weld micro-leaks in a data centre